Size Downstream Over-Speed & Buffer Length Using V-Curve Physics
If your primary filler runs 120 packs/min and your downstream case packer is also capped at 120 packs/min, any 60-second carton magazine reload creates a 120-pack backlog that can never be cleared without stopping the primary filler! Grounded in line sizing and turnkey planning and system integration and line balancing, downstream machines need both an accumulation buffer (N_buf) and a catch-up speed delta (V_sec - V_prim).
Use the two engineering formulas below: N_buf = V_prim × T_stop_min (packs to absorb one minor downstream stop) and T_drain = N_buf / (V_sec - V_prim) (minutes required to empty the buffer before the next stop).
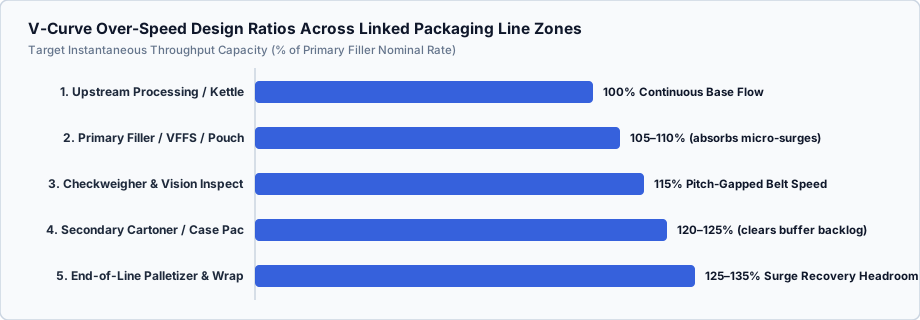
Worked V-Curve & Buffer Sizing Reference Table
Pre-calculated V-curve speeds and FIFO buffer capacities for 60–240 BPM primary lines (assuming 1.0 min minor downstream stop):
| Primary Rate (V_prim) | Inspection (115%) | Case / Cartoner (122%) | Palletizer (130%) | 1-Min Buffer & Drain Time |
|---|---|---|---|---|
| 60 packs/min | 69 PPM | 74 PPM eq. | 78 PPM eq. | 60 packs -> drains in 4.3 min |
| 100 packs/min | 115 PPM | 122 PPM eq. | 130 PPM eq. | 100 packs -> drains in 4.5 min |
| 140 packs/min | 161 PPM | 171 PPM eq. | 182 PPM eq. | 140 packs -> drains in 4.5 min |
| 240 packs/min | 276 PPM | 293 PPM eq. | 312 PPM eq. | 240 packs -> drains in 4.5 min |
Next, model headcount and OEE financial returns in our end-of-line ROI estimator.
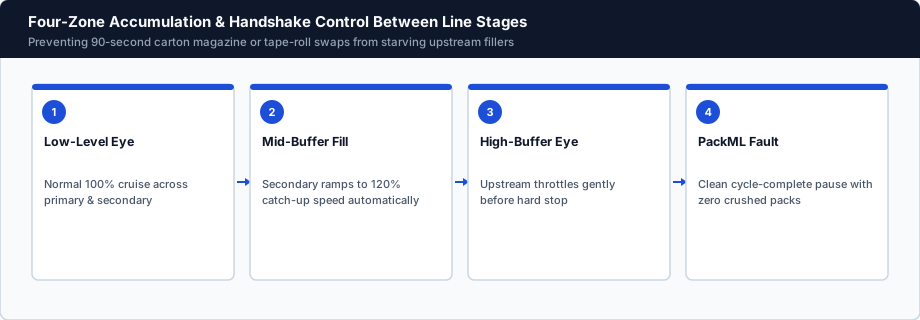
System Integration Engineering Notes
- Converting Pack Count to Conveyor Length: For single-file FIFO pouches of pitch
P_mm(pack length + 50 mm gap), linear buffer lengthL_m = (N_buf × P_mm) / 1000. Above 8–10 m, switch to multi-lane mass flow or vertical gondola buffers. - Series Availability Multiplier Check: Unbuffered 4-machine line at 93% each =
74.8%OEE; decoupling the case packer + palletizer with a 90-second buffer lifts effective system availability above88–90%. - Never Undersize the Case Erector: If 12 pouches fill one case at 140 pouches/min (
11.7 cases/min), specify a15–18 cases/minerector-packer, never a12 cases/minborderline unit.
Validate Your Line Balance With Our Systems Engineers
Send your SKU counts per case, primary BPM, and available hall length via Project Brief.
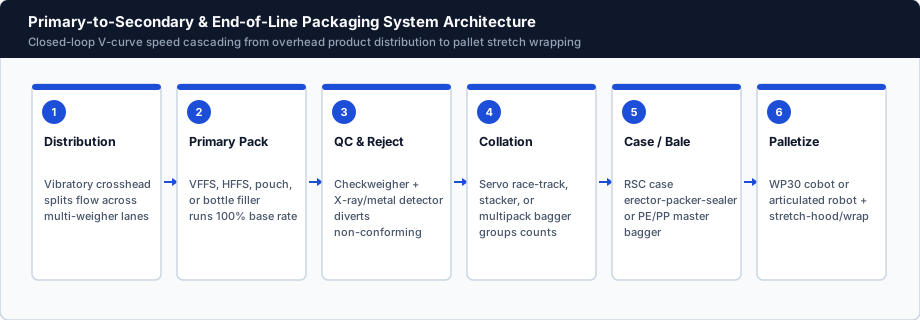
Explore related system modules in Packaging Line Systems, Line Balancing & OEE Specs, or send your floorplan & target BPM via Project Brief.
Related Specifications
Further Reference
Request Project Configuration Review
Share layout constraints, architectural drawings, or throughput targets with Packaging Line Systems Technical Group.
Review My Line Layout