Zero-Starvation Distribution From Fryer/Roaster to Pallet
In high-volume snack, nut, cereal, frozen-food, and pet-kibble halls, running 3 to 6 primary baggers from separate forklift tote dumps wastes floor space and causes chronic weigher starvation. Grounded in industry line blueprints and system integration and line balancing, overhead proportioning vibratory distribution galleries feed every multihead weigher on demand via motorized bias gates.
Reference multi-machine snack lines pair twin-discharge MBP 16C3 DMA multihead weighers over five RQ550 120 BPM pillow baggers (30 g), cascading directly into three R800 secondary multipack baggers (180 g) or high-speed gravity case packers.
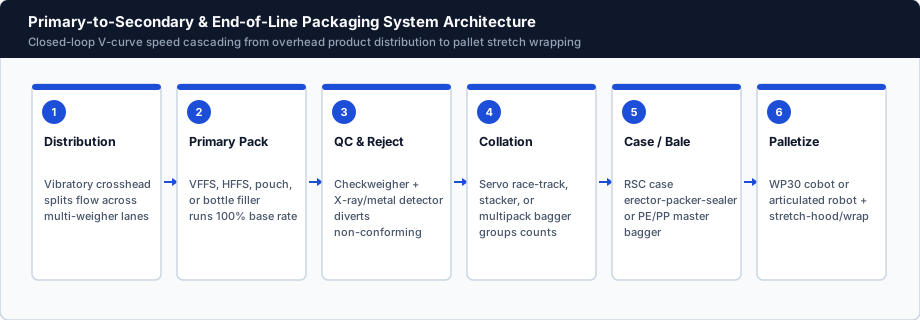
Multi-Bagger Snack & Granule System Station Specs
End-to-end equipment specification from product elevation to stretch-wrapped pallet:
| Line Zone | Equipment Specification | Design Capacity | Sanitary / Quality Detail |
|---|---|---|---|
| 1. Product Elevation & Split | Z-bucket / Swan-neck + electromagnetic vibratory gallery | 500 – 4,500 kg/hr | Tool-free drop-bottom wipe-down pans |
| 2. Multihead + Primary Bagger | 14/16/24-head dimple weigher + 120–140 BPM VFFS / poucher | 60 – 140 BPM per lane | N2 flush <1.5% O2 + jaw product-in-seal detect |
| 3. Single-Bag QC & Flatten | Combo checkweigher + metal detector + spring belt flattener | 115% belt pitch speed | Lockable air-blast / drop-flap reject |
| 4. Secondary & Palletizing | R800 multipack bagger OR gravity RSC drop packer + robot | 120–130% V-curve surge | Soft-drop cushioning protects fragile crisps |
Check ceiling height and buffer spacing with our line balancing and buffer calculator.
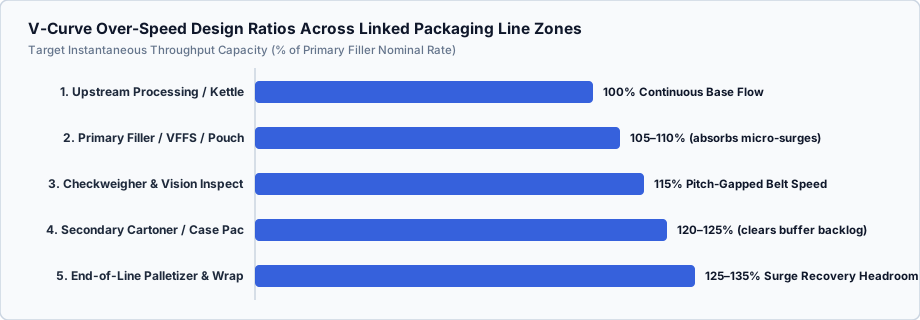
System Integration Engineering Notes
- First-In, First-Out Crosshead Recycling Loop: Size distribution pan flow 10% above combined weigher draw with a gentle return loop or proportional end-gate sharing so Seasoned snacks never segregate.
- Shared Rigid Structural Mezzanine: Isolate multihead weigher support columns from VFFS and walkway vibration frames so operator footsteps never corrupt
±0.5 gload-cell readings. - Quick-Swap Twin-Tube / Single-Tube Flexibility: Run twin small snack bags on weekdays and swap forming collars to club-size 500 g pillow bags in 25 minutes.
Request a Multi-Weigher Hall Layout
Send number of baggers, product bulk density, bag weights, and ceiling height via Project Brief.
Explore related system modules in Packaging Line Systems, Line Balancing & OEE Specs, or send your floorplan & target BPM via Project Brief.
Related Specifications
Further Reference
Request Project Configuration Review
Share layout constraints, architectural drawings, or throughput targets with Packaging Line Systems Technical Group.
Review My Line Layout