Why Standalone Machines Underperform Without System-Level Engineering
Buying fast standalone primary fillers and bolting them together with generic conveyors rarely delivers rated factory output. Whenever a carton magazine runs low, a tape head jams for 60 seconds, or an operator pauses to stack shipping cases, unbuffered lines cascade backward and shut down primary dosing. True packaging line systems engineer the entire plant floor—from overhead product distribution and primary bagging/bottling through inline inspection, secondary collation, case/bale containment, and palletizing—around a unified V-curve speed cascade and PackML state control.
Across modern snack, powder, dairy, personal-care, and chemical plants, integrating automated secondary and end-of-line packaging downstream of 120–140 BPM primary cells cuts manual packing labor by 30–40% while lifting shift OEE by up to 25%.
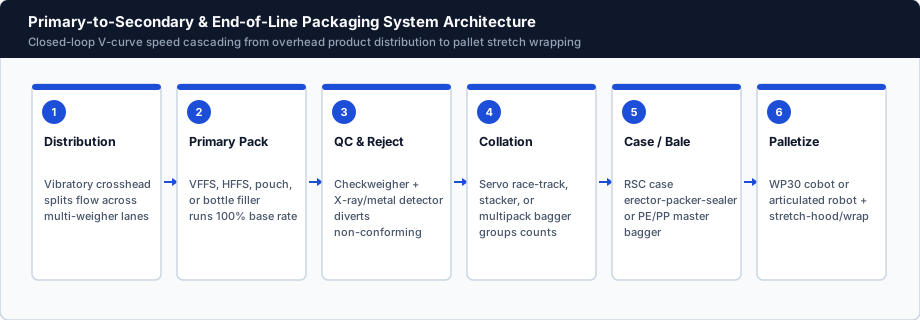
System Sub-Assemblies & Speed-Cascade Architecture
Core functional zones across turnkey primary-to-pallet packaging line systems:
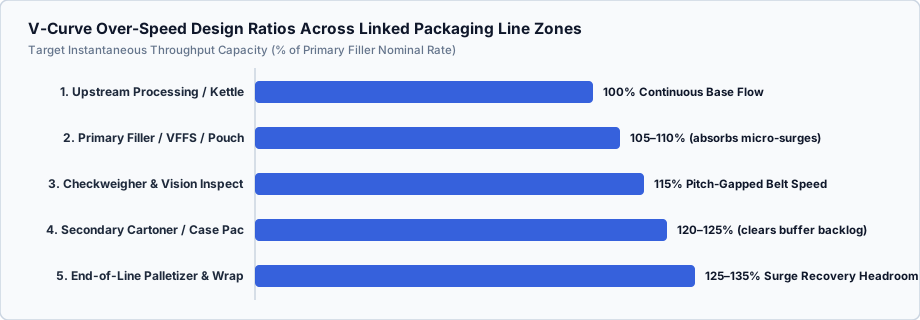
| System Tier | Core Equipment Modules | Design Speed Ratio | Primary Engineering Objective |
|---|---|---|---|
| Upstream Distribution | Crosshead vibratory conveyors, CLP-650 unscramblers | 105% on-demand feed | Zero-starvation multi-lane balancing |
| Primary Containment | Multihead VFFS (120–140 BPM), HFFS, 6–16 head fillers | 100%–108% anchor | Hermetic seal + ±0.2%–1.0% dose accuracy |
| Inline Inspection | Dynamic checkweigher, metal detector, X-ray, vision | 115% pitch-gapped | Lockable reject verification before cartoning |
| Secondary Packaging | Cartoners, RSC/SRP case packers, multipack/master baggers | 120%–125% catch-up | Drain accumulation buffer after magazine swaps |
| End-of-Line Logistics | WP30 cobot / 4-axis robot palletizer + stretch wrapper | 125%–135% surge | Forklift-ready GS1-labeled unit loads |
Explore downstream case/pallet modules in end-of-line packaging systems, collation cells in secondary multipack and cartoning, and V-curve math in system integration and line balancing.
System Integration Engineering Notes
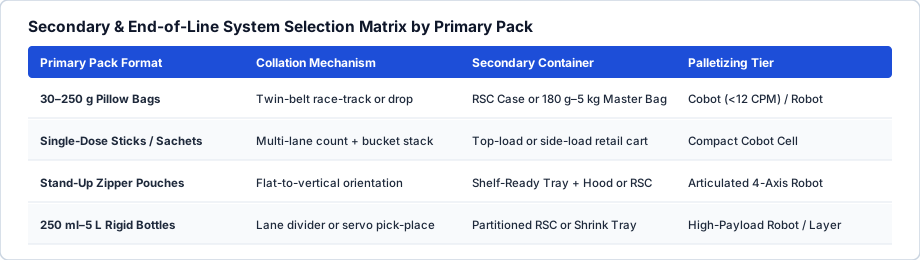
- Multi-Primary Into Multi-Secondary Topology: High-output snack halls route five 120 BPM primary pillow-pack VFFS machines (30 g) directly into three secondary multipack baggers (180 g) via overhead distribution without manual tote handling.
- Single-Vendor Factory Acceptance Test (FAT): Assembling and dry/wet cycling the full linked line on one test bay catches transfer-plate snags, photoeye reflections, and PLC handshake race conditions before ocean freight.
- Recipe-Driven Format Changeover: Master HMI recipe selection propagates belt speeds, reject weight windows, and pallet patterns simultaneously across linked stations.
Four Plant Constraints Shape Every System Layout
Share your primary pack format & target units/minute, secondary case/bale count, pallet height/footprint, and available hall dimensions (L × W × ceiling clearance).
Submit your floorplan constraints via Project Brief or compare sector blueprints in industry line blueprints.
Explore related system modules in Packaging Line Systems, Line Balancing & OEE Specs, or send your floorplan & target BPM via Project Brief.
In This Section
Further Reference
Request Project Configuration Review
Share layout constraints, architectural drawings, or throughput targets with Packaging Line Systems Technical Group.
Review My Line Layout