Test Fault Recovery & Changeovers—Not Just 5 Minutes of Perfect Running
Testing each machine separately for 10 minutes proves almost nothing about how a linked system behaves on a Tuesday night shift! Grounded in line sizing and turnkey planning and system integration and line balancing, a rigorous linked Factory Acceptance Test (FAT) deliberately injects downstream micro-stops, underweight packs, missing foil caps, and SKU changeovers while measuring sustained OEE.
Include the six linked qualification tests below directly in your procurement URS before paying milestone deposits.
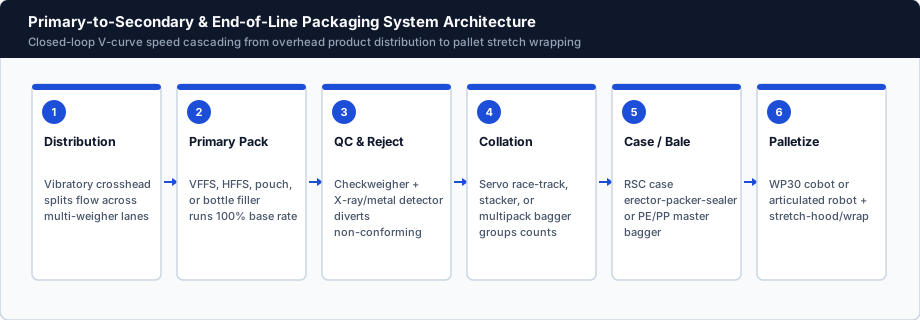
Six-Point Linked Packaging Line FAT Protocol
Mandatory acceptance tests before crating a multi-machine system:
| FAT Test Phase | Test Procedure | Pass / Acceptance Threshold |
|---|---|---|
| 1. Sustained Linked Run | 60–120 min continuous run on production materials | >=95% net good output at rated primary BPM |
| 2. Simulated Downstream Stop | Hold case packer/cartoner paused for 60 seconds | Buffer absorbs surge; drains cleanly with 0 stops |
| 3. Challenge Test Pack Reject | Feed Fe/Non-Fe/SS + +/- weight + bad-code packs | 100% into locked reject bin; 0 into secondary case |
| 4. Worst-Case SKU Changeover | Swap smallest pouch/bottle to largest + new case | Completed within <=20–30 min target; 1st case square |
| 5. Safety & E-Stop Zoning | Open guard doors & pull zone E-stops under load | Safe Category-3/PLd stop; clean PackML restart |
| 6. Utility & Noise Audit | Measure peak kW, CFM/m³/min air, and dB(A) @ 1 m | Matches URS facility header ratings (<78–80 dB) |
See how our engineering team executes full-floor testing on packaging line system integrator.
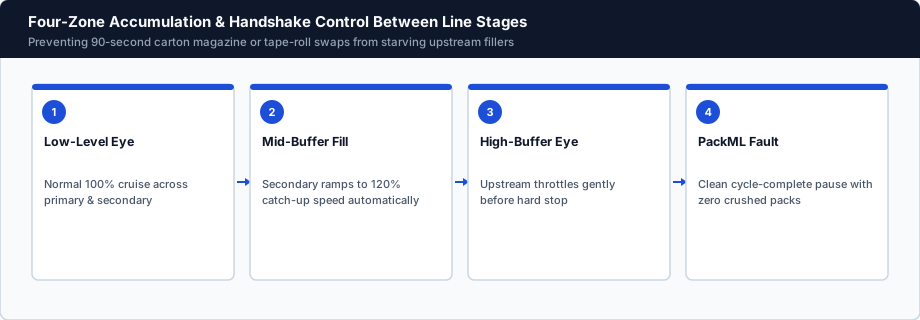
System Integration Engineering Notes
- Ship Production Corrugated, Film & Product: Never let a line FAT run only on empty cartons or wooden dummy blocks—real product center-of-gravity and corrugated board flute stiffness expose every transfer quirk.
- Video-Recorded Changeover SOPs: Film the lead technician executing the SKU changeover during FAT—that annotated video becomes your instant training manual at SAT.
- Pre-Numbered Split-Line Match Marks: Before unbolting conveyors for container shipping, stamp laser/engraved match marks and plug labels on every frame joint.
Share Your URS for Technical Line Review
Upload or paste your project requirements via Project Brief.
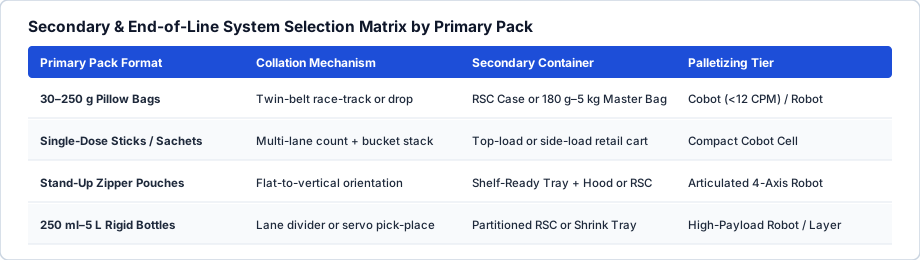
Explore related system modules in Packaging Line Systems, Line Balancing & OEE Specs, or send your floorplan & target BPM via Project Brief.
Related Specifications
Further Reference
Request Project Configuration Review
Share layout constraints, architectural drawings, or throughput targets with Packaging Line Systems Technical Group.
Review My Line Layout